Requirements for the use of cemented carbide roller rings
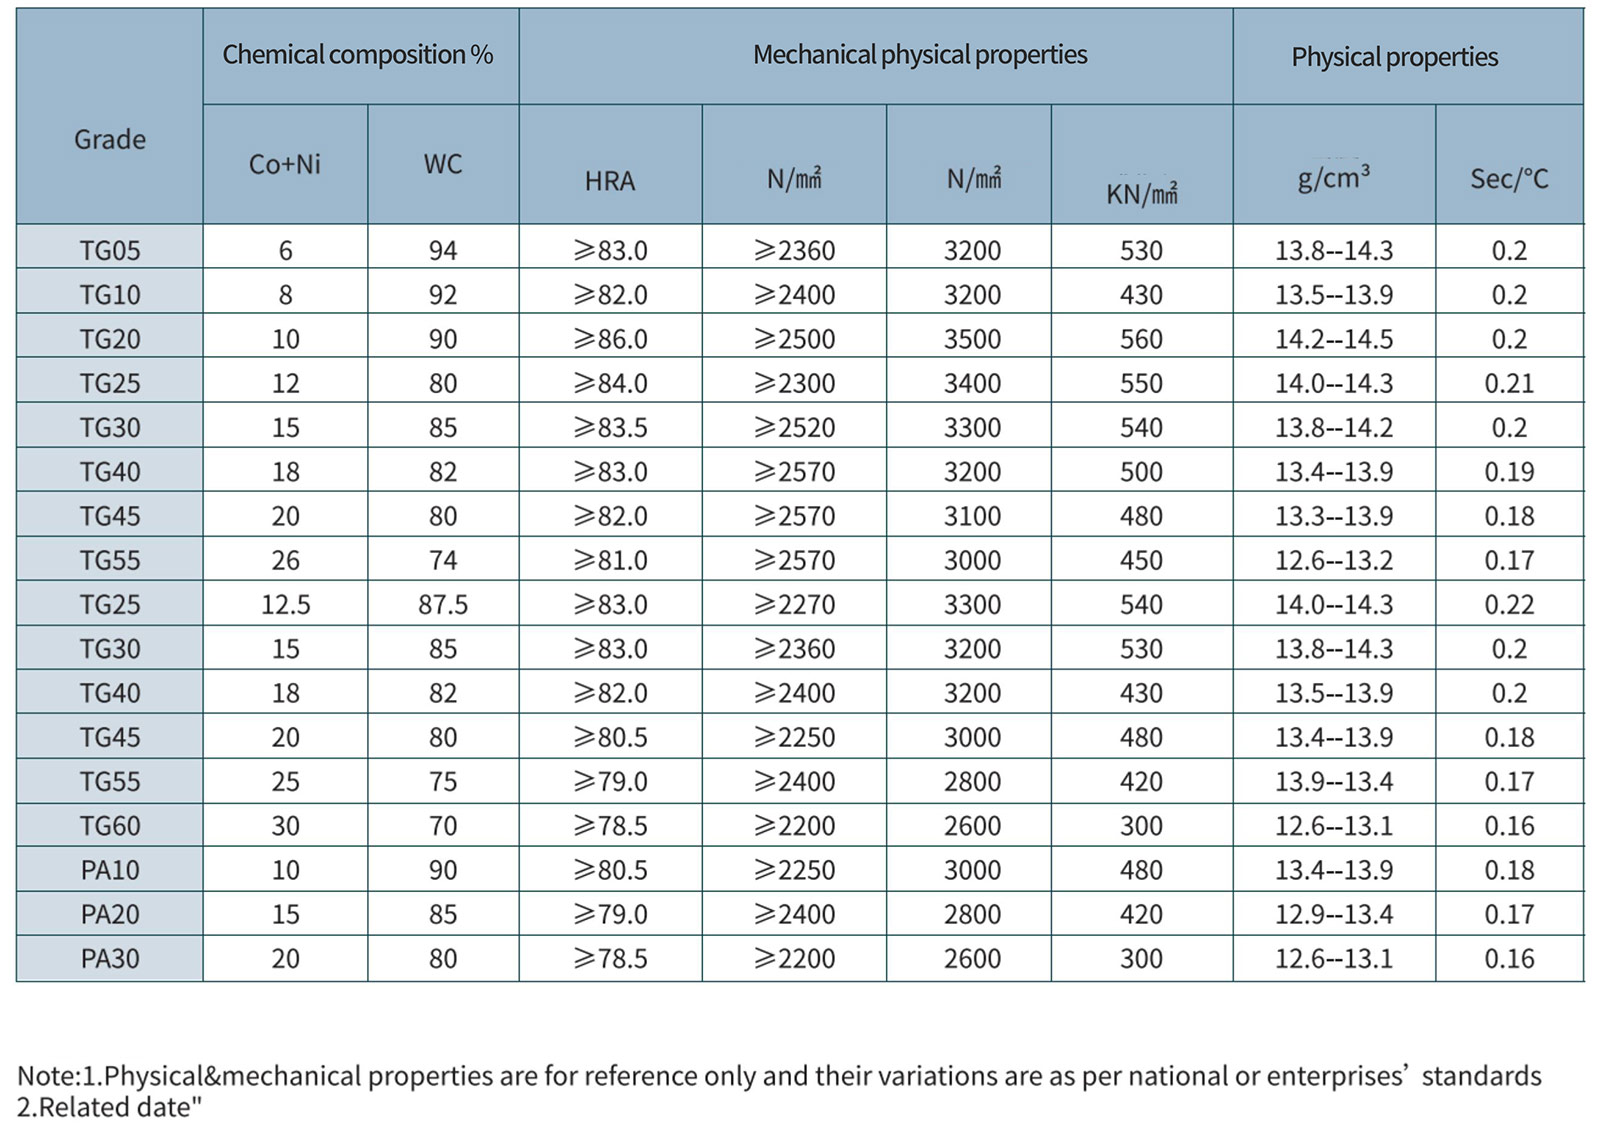
Cemented carbide roll ring is a kind of tool material which consists of tungsten carbide and cobalt with high hardness and wear resistance.To take advantage of high wear resistance,long life and high efficiency of cemented carbide roll rings during the high speed rolling,attention should be paid as follows when purchasing and using cemented carbide roll rings.
1、Grades selection
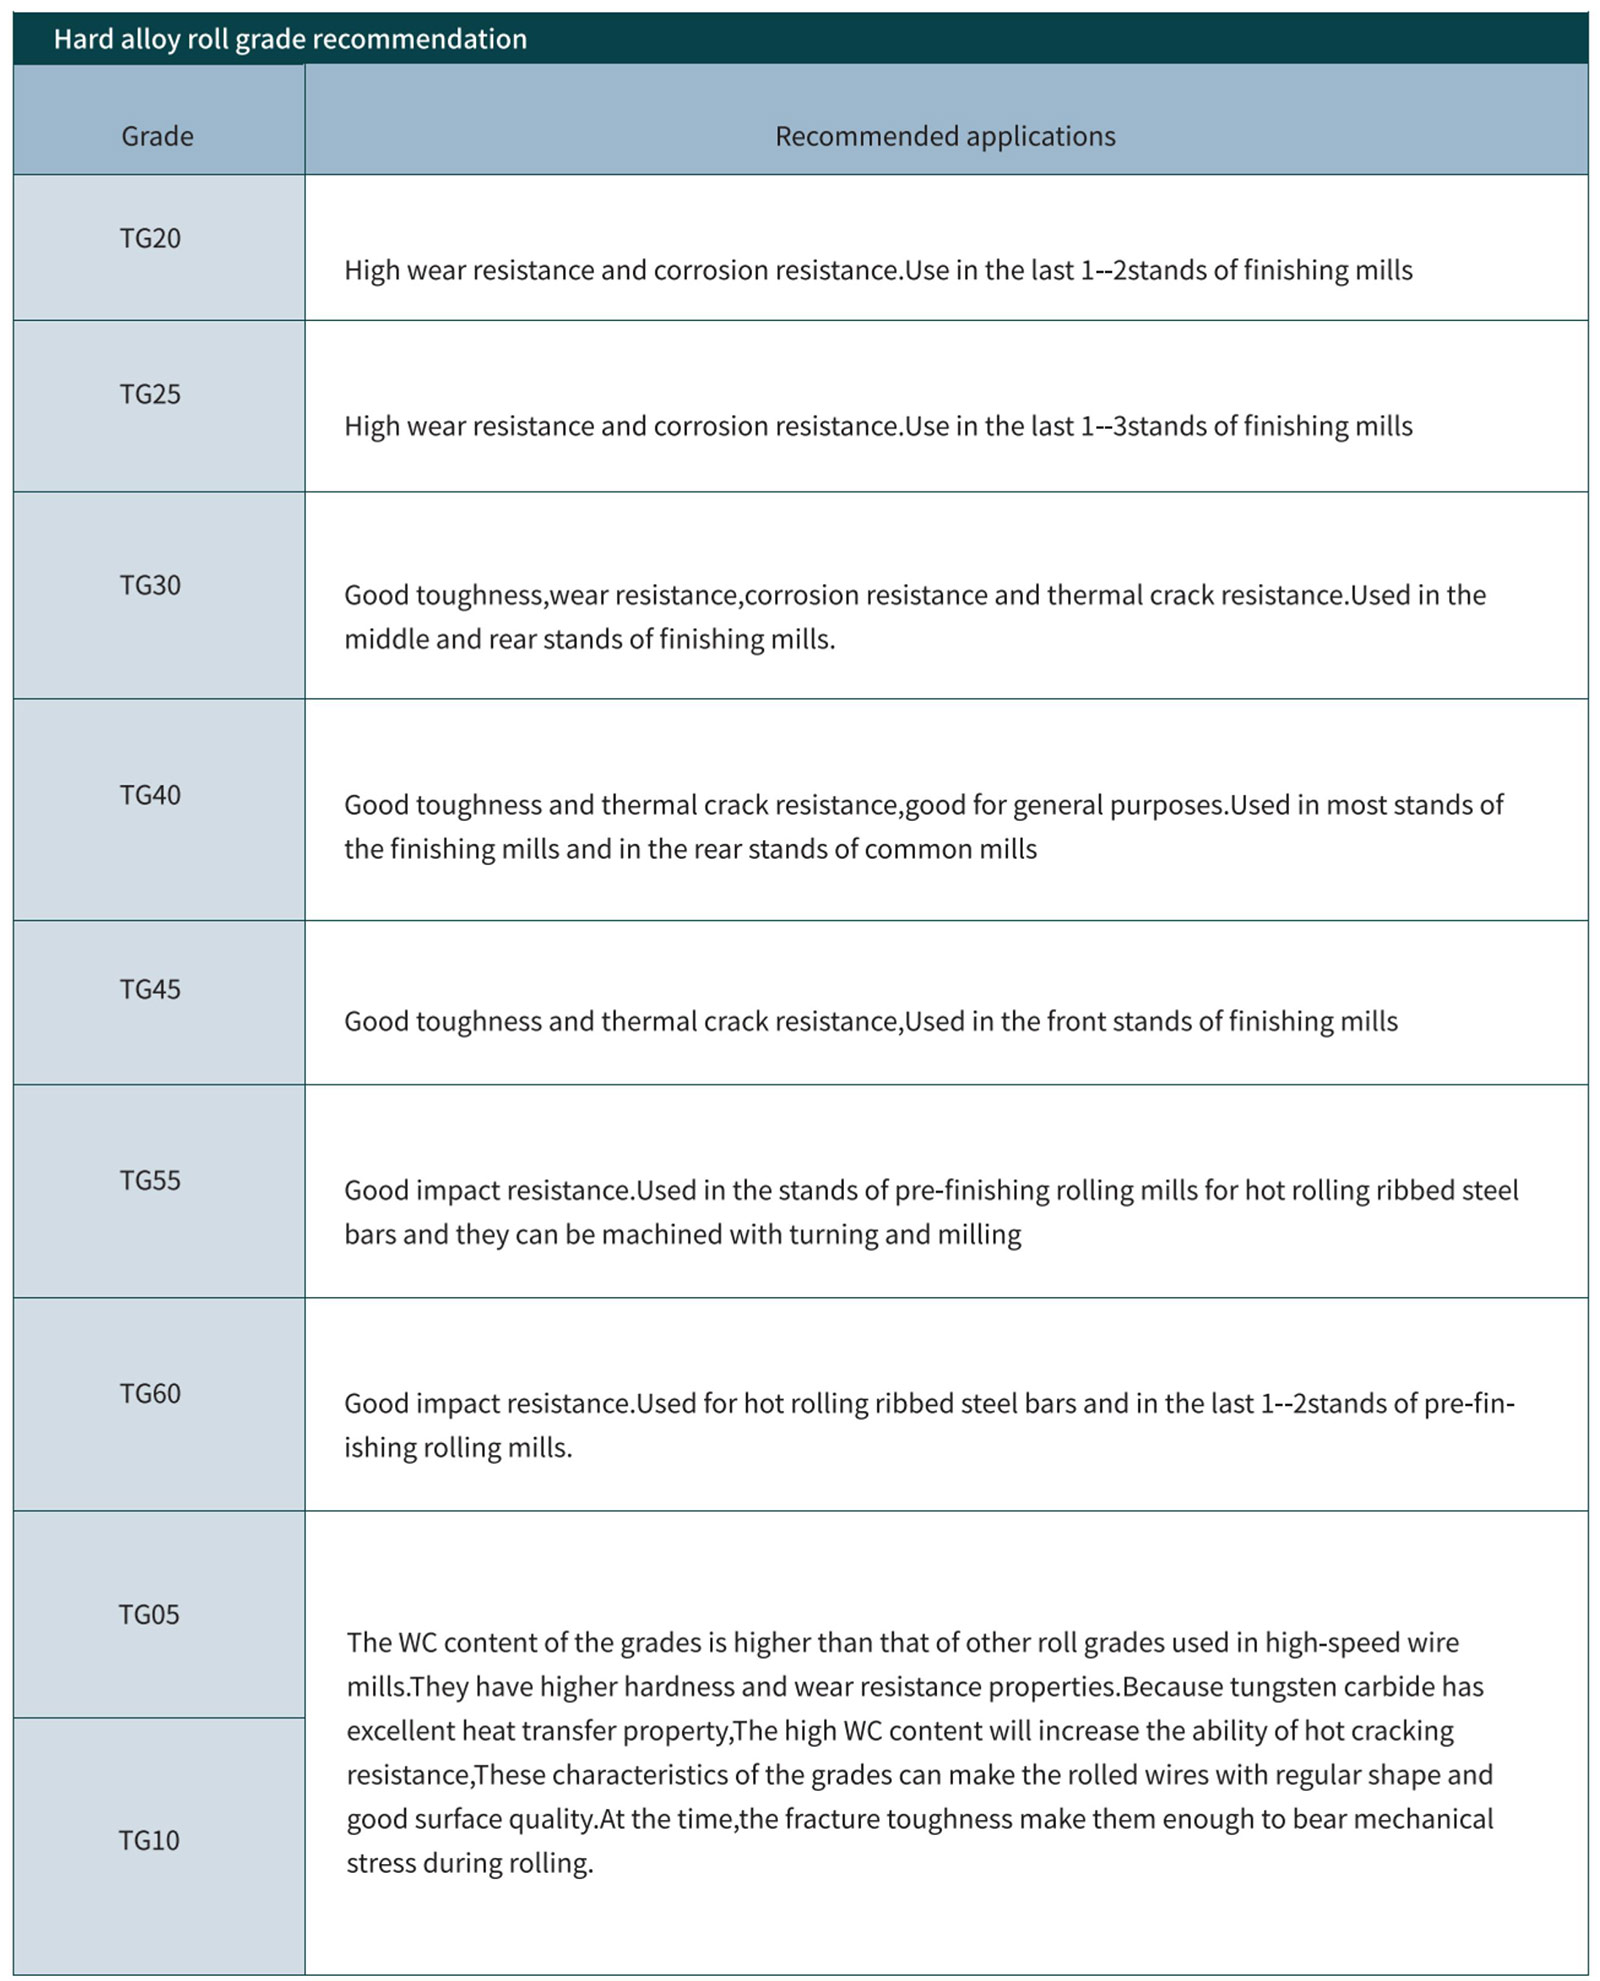
An overall understanding of cemented carbide grades is a basis for correctly selecting the grades for roll rings used in the stands of rolling mills and an optimal combination of grades is required for the various stands of rolling mills.
Steel-case mounting and assembly of roll rings should be strictly performed according to the precision required by the design process.Proper fitting is needed for the roll rings,roll mandrel for stands and conical sleeves,which can not be over tight or loose,When it is too tight,the roll rings are in a tensile state and more fluctuation of rolling force will make the roll rings break.When it is loose,it causes leads the roll rings,roll mandrel and conical sleeve to slide relatively during rolling,which scratches conical sleeves and roll mandrel so resulting in cracks.Before running the mill make a check if the roll rings meets the needs and roll rings,the assembling faces of the conical sleeve and the roll mandrel need to be cleaned.It is forbidden to
knock at the roll rings with a hammer or other hard materials when running the mill.It is forbidden for the roll rings to impact each other during the transportation and installation to prevent roll rings from damage.
Coolingi intended to reduce the influence on rollrings of thermal corrosion,fatigue and stress during miling.It can prevent the roll rings from
cracking and slow down the diffusion of cracks,prolong the life time of grooves,It plays an important role in optimizing the performances of roll rings.The reference date for cooling are as follows:The temperature of cooling water is below 25℃,pressure of cooling water is 5-6 bar with a water volume of 24-30m³/hr/stand,The water is jetted in a radial direction and the angle between the waterjet and the rotating direction of roll rings is 15-30 degrees.The width of the water column is 2 times that of the groove and the water should be jetted directly into the grooves and the water
Water quality requirement:ForYGH series PH≥7.2medium or weak alkali water,ForYGR series PH≥7.2medium or weak alkali water or PH≤
7.2weak acid water,The content of solid particles in the water<15milligram/litre
4、Reasonable rolled quantity
During rolling microcracks in grooves can not be avoided,and they need to be reground when they are at a certain depth (normally controlled at 0.2mm).Excessrolling causes the depth of microcracks to extend rapidly and dangers of crushed rols increase,which should be prevented.The volume of material to be rolled normally after each regrinding is as follows.
5、Regrinding of grooves
Microcracks will occur after the rolling of the groove for some time and when the microracks extend to 0.2mm the roll ring has to be reground .Microcracks must be reground thoroughly when regrinding,otherwise the unground microcracks will make the microracks extend more rapidly during the next rolling and probably make the roll ring crack.The recommended amount of regrinding after normal rolling is as follows.
Roll rings for stands 9-10 of finishing rolling mill(0.4--0.6)mm
Roll rings for stands 1--8 of finishing rolling mill(0.7--1.2)mm
Roll rings for stands of pre-finishing rolling mill 91.2--2.0)mm
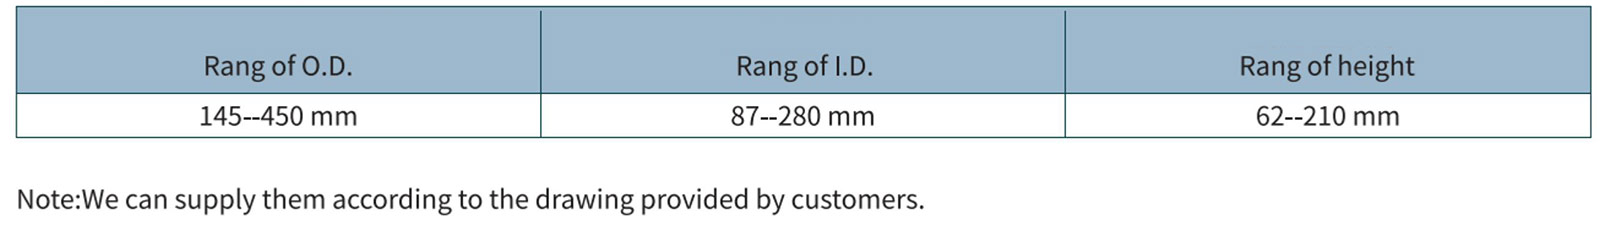
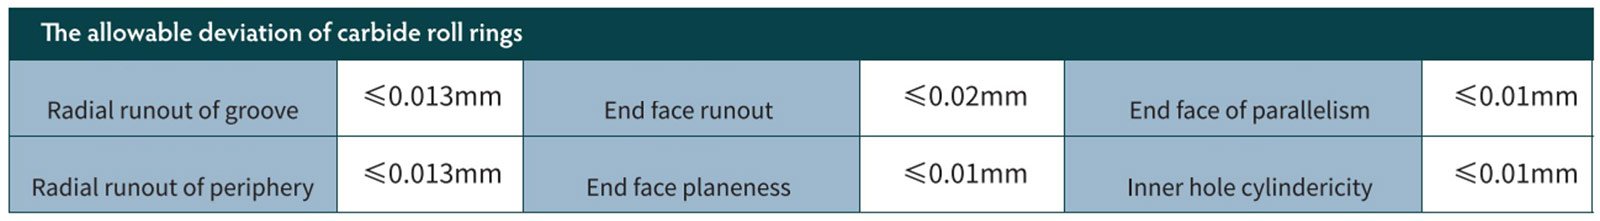
6、The allowable deviation of carbide roll rings
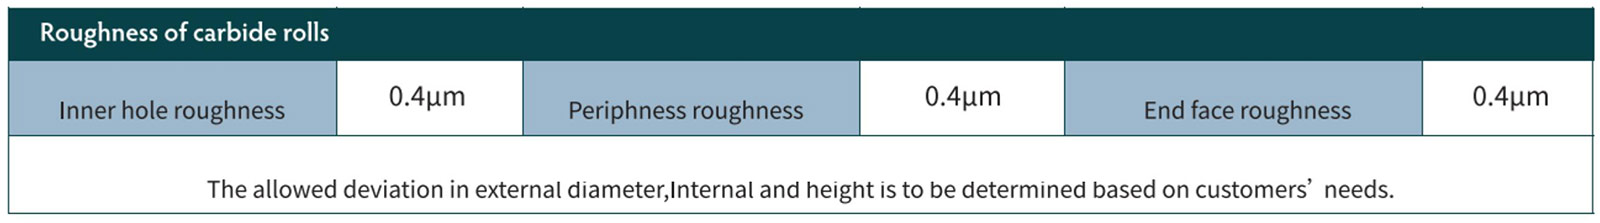
7、Roughness of carbide rolls